Enhance product safety and quality control
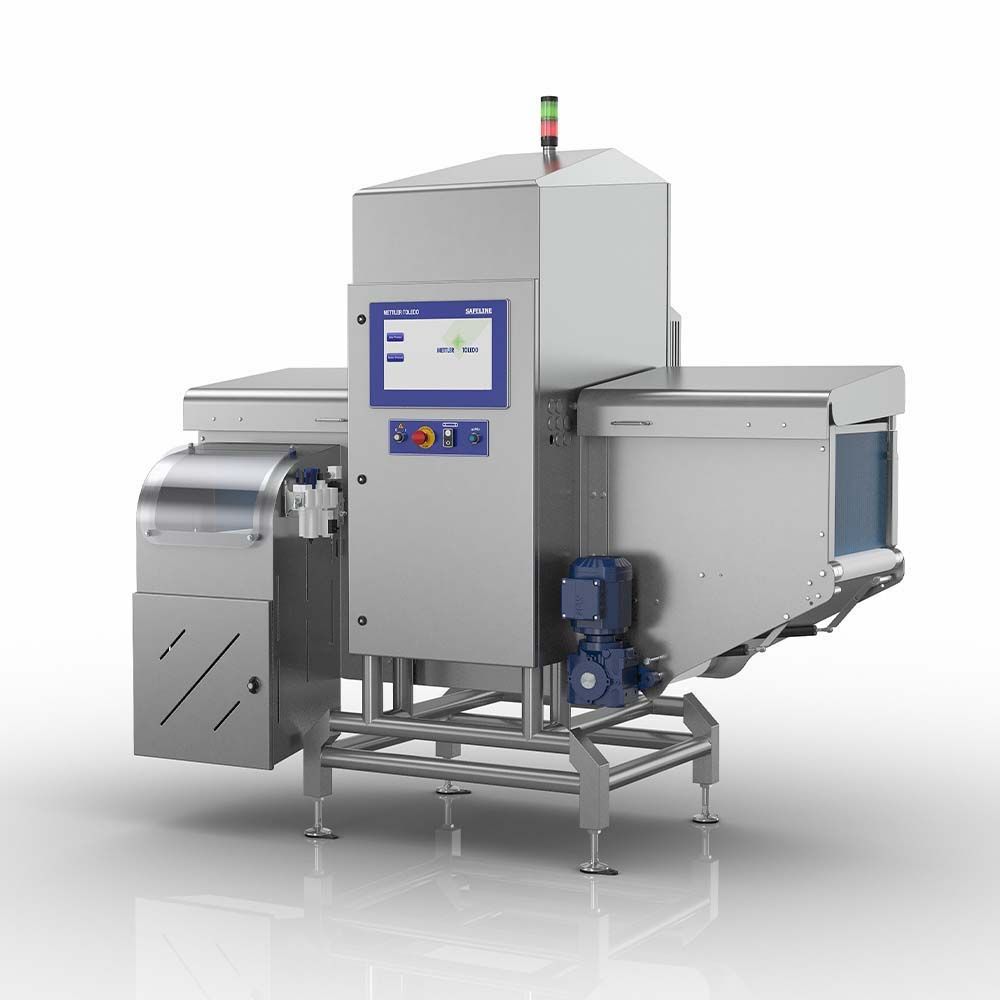
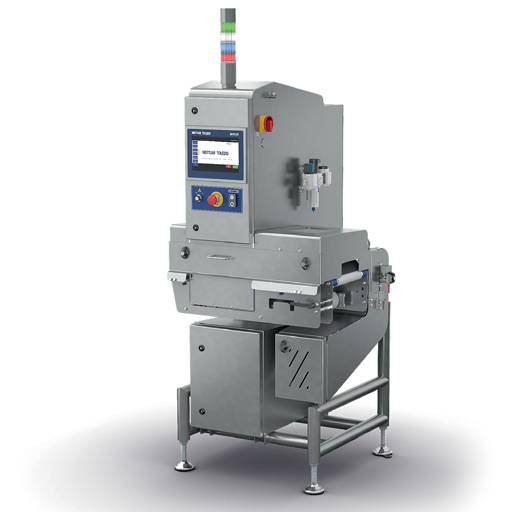
Inline industrial X-ray inspection systems are designed to detect unwanted physical contaminants in food and pharmaceutical products, regardless of product shape, density or packaging format.
These advanced x-ray inspection systems offer maximum contamination detection sensitivity for a diverse range of food and pharmaceutical applications in various types of retail packaging.
Safeline industrial x-ray systems from Mettler Toledo can identify dense foreign bodies or material contaminants such as glass, metal, mineral stone and calcified bone, even when they are hidden inside complex products or packaging formats. This helps manufacturers protect consumers and safeguard brand reputation, and maintain compliance with retailer codes of practice and global safety standards
X-ray Inspection systems ensure product safety and assurance for:
- Packaged food and pharmaceutical products
- Products packaged in glass jars and bottles
- Metal cans and foil packaging
- Bulk flow (loose) food products prior to packaging
- Pumped products including meat, poultry, slurries, semi-solids and liquids
- Unpackaged food products
X-ray inspection for Food Manufacturers
In addition, to contaminant detection, X-ray inspection systems support quality control processes. These include integrity inspections such as verifying fill levels, controlling portion size, inspecting seal integrity and detecting packaging defects.
This multi-functional inspection capability plays a critical role in helping food manufacturers meet strict food and safety regulations and maintain consistent product quality.