Product Inspection Solutions

Inspect. Protect. Comply

Product inspection systems enable manufacturers to inspect every product with confidence, ensuring consistent quality across food, pharmaceutical, chemical and industrial production  lines.

Designed for high-speed, high-performance production environments, our advanced inline inspection solutions help you enhance product safety, strengthen quality control, improve operational efficiency, and comply with stringent industry regulations, while protecting your brand and profitability.

Our comprehensive range of industrial product inspection equipment includes:

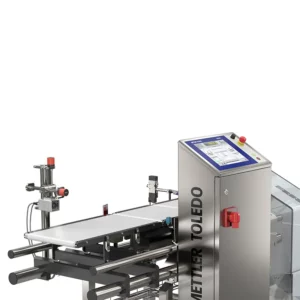
  • Dynamic checkweighers for accurate in-line weight control and reduced product giveaway
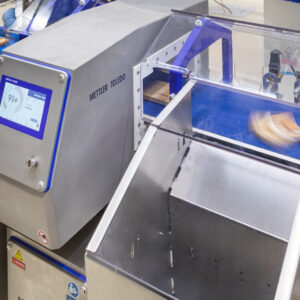
  • Industrial metal detection systems to detect and reject metal contaminants
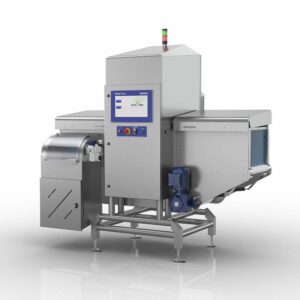
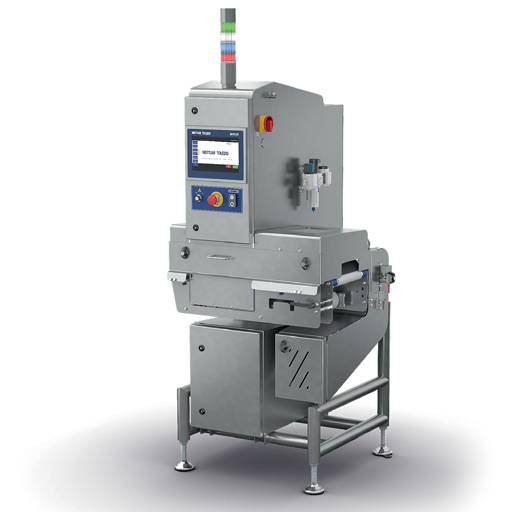
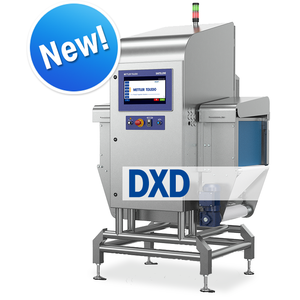
  • X-ray inspection systems for contaminant detection and product integrity checks
  • Vision inspection systems for label verification, code inspection, and packaging quality control
  • Combination inspection systems combine precise weighing with metal detection, x-ray inspection or vision inspection for enhanced product quality and safety


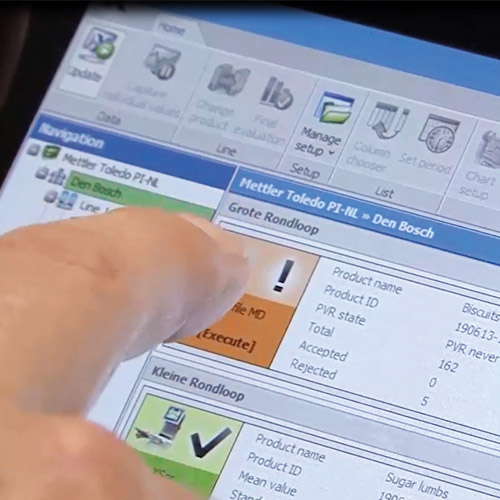
These systems can operate as stand-alone inspection units or be fully integrated into automated production lines using state-of-the-art inspection software to provide enhanced data management, traceability, and process control.

Applications: Product Inspection, Food Manufacturing, Pharmaceutical Manufacturing, Chemical Industry, Non-Food Industries, Metal Detection Systems, X-Ray Inspection Systems, Checkweighers

Share:

All Product Inspection Solutions Items

Product inspection solutions encompass a variety of technologies and methodologies used to ensure the quality, safety, and compliance of manufactured products across various industries. These solutions are essential for detecting defects, contaminants, and deviations from specifications throughout the production process. Here are some key product inspection solutions:

1. Visual Inspection Systems:

  • Automated Visual Inspection (AVI): Uses cameras and image processing software to detect defects such as scratches, cracks, or misalignments on products.
  • Machine Vision Systems: Analyze images of products to ensure they meet predetermined criteria for quality, shape, and consistency.

2. X-ray Inspection Systems:

  • X-ray Inspection: Utilizes X-ray technology to detect contaminants, foreign objects, or defects within products, including food, pharmaceuticals, and packaged goods.
  • X-ray Computed Tomography (CT): Provides detailed 3D images of internal structures, allowing for thorough inspection of complex products or assemblies.

3. Metal Detection Systems:

  • Metal Detectors: Identify metallic contaminants in food products, pharmaceuticals, and other packaged goods to prevent contamination and ensure consumer safety.
  • Magnetic Separators: Remove ferrous contaminants from powders, liquids, and bulk materials during production processes.

4. Checkweighers:

  • Dynamic Checkweighing: Weighs products in motion to ensure they meet specified weight criteria, helping to prevent underfilled or overfilled packages.
  • Inline Checkweighers: Integrated into production lines for real-time weight verification and rejection of non-compliant products.
Why Choose Our Product Inspection Equipment?

METTLER TOLEDO Product Inspection systems include both stand-alone and fully integrated automated inspection technologies, designed to enhance productivity and ensure product quality and safety for manufacturers in the food, pharmaceutical, chemical, and other non-food industries.

Our inspection technologies are engineered to:

  • Protect your brand and consumers with advanced contamination detection and quality assurance systems
  • Improve productivity and reduce downtime in high-speed production environments
  • Support compliance with industry regulations, retailer standards, and global food safety legislation
  • Deliver reliable, repeatable performance in demanding manufacturing conditions


By implementing high-performance product inspection systems, manufacturers can minimize product recalls, reduce waste, improve profitability, and maintain the highest standards of product integrity.


"*" indicates required fields

This field is for validation purposes and should be left unchanged.
Name*